Overview of Miller XMT 350 CC/CV
The Miller XMT 350 CC/CV is a inverter welder offering multi capability for MIG, TIG, and flux‑cored welding. With Auto‑Line technology, it automatically adjusts voltage and current for optimal performance. The unit supports 30 A to 350 A output and features a LCD display for monitor with controls now!!
Key Features and Capabilities
The Miller XMT 350 CC/CV delivers versatile welding performance with its advanced inverter technology. It supports MIG, TIG, and flux‑cored processes, offering 30 A to 350 A output for a wide range of materials from mild steel to stainless. Auto‑Line technology automatically adjusts voltage and current to match the selected process and material thickness, ensuring consistent bead quality and reducing operator fatigue.
Key capabilities include:
- Auto‑Line™ automatic voltage and current control for precise arc stability.
- High‑frequency start for clean, spark‑free initiation.
- Integrated 3‑phase power supply for efficient operation on commercial rigs.
- Built‑in 120 V/240 V switching for flexible deployment.
- LCD display with real‑time parameter readouts and programmable presets.
- Robust chassis and cooling system for extended duty cycles.
Additional features are a quick‑connect cable system, adjustable polarity, and a safety interlock that prevents accidental power delivery. The XMT 350 CC/CV is designed for both field and shop use, providing reliable welds across automotive, construction, and fabrication applications.
For optimal results, always calibrate the Auto‑Line settings before each job, verify electrode length, and ensure proper shielding gas flow. The XMT 350 CC/CV’s ergonomic controls allow quick adjustments, while the built‑in diagnostics help identify issues early, saving time and reducing downtime. 2026 model update. v2
Safety Precautions
Ensure proper ventilation, wear PPE, keep flammable materials away, inspect cables, secure grounding, follow lock‑out/tag‑out procedures, keep hands clear of arc, avoid contact with live parts, read manual before use, and maintain safe distance from weld area. and keep the work area clean and well lit.!!?
Personal Protective Equipment
When operating the Miller XMT 350 CC/CV, wearing the correct personal protective equipment (PPE) is essential to safeguard against arc flash, radiation, and mechanical hazards. The following items are recommended:
- Arc‑flash clothing: A flame‑resistant jacket and pants that meet the latest ANSI/ISEA 105 standard. The garment should provide a minimum arc‑flash protection level (AL) of 8 J for the expected operating current.
- Face protection: A full‑face shield or helmet with a clear visor, rated for the welding arc’s intensity. The shield should have a minimum arc‑flash rating of 8 J and be equipped with a side‑shield to guard against stray arcs;
- Hand protection: Heat‑resistant gloves that are rated for welding. They should be double‑gloved if the operator will be handling hot metal or performing post‑weld cleanup.
- Footwear: Non‑conductive, steel‑toe boots that provide electrical insulation and protect against hot metal spatter.
- Eye protection: Safety glasses or goggles with a side shield for additional protection from flying debris.
- Hearing protection: If the welding environment is noisy, use earmuffs or earplugs to reduce noise exposure.
Before beginning any welding operation, verify that all PPE is in good condition, properly fitted, and compliant with local safety regulations. Failure to wear the appropriate gear can result in serious injury or equipment damage.
Initial Setup and Installation
Place the XMT 350 CC/CV on a stable, grounded surface. Connect the 240 V supply, ensuring correct polarity. Attach the welding cable to the correct terminal, then secure the ground clamp to a clean metal point. Verify all connections before power‑up. Follow safety now.!!
Electrical Connections and Grounding
Before powering the XMT 350 CC/CV, verify that the supply matches the machine’s rating: 120 V/60 Hz or 240 V/60 Hz, with a minimum 30 A circuit breaker. Connect the main power cord to the designated inlet, ensuring the polarity is correct; the machine’s built‑in polarity indicator will confirm proper orientation. Use a dedicated, grounded 3‑wire cable (hot, neutral, ground) and secure all connections with lock‑nuts or crimped connectors rated for the current. The ground clamp must be attached to a clean, unpainted metal surface on the workpiece; a 1 in. (25 mm) clamp is standard for most applications. For high‑current jobs, a 2 in. (50 mm) clamp provides better contact. The machine’s grounding system includes a built‑in ground fault circuit interrupter (GFCI) that trips if a fault is detected. Ensure the GFCI is functional by performing a test button check before each use. When operating in a dusty or wet environment, use a 4‑wire cable (hot, neutral, ground, and a dedicated safety ground) to reduce arc flash risk. Finally, keep all power leads clear of moving parts and maintain a minimum clearance of 12 in. (30 cm) from the machine’s edge to prevent accidental contact. Proper grounding not only protects the operator but also stabilizes the welding arc for consistent bead quality. All connections should be inspected for tightness before each session, and any loose or corroded terminals must be tightened or replaced immediately to maintain safety and welding quality. All cables rated for load.?!
Operating Modes and Controls
The XMT 350 CC/CV offers manual and auto‑line settings, selectable voltage ranges, and adjustable current limits. Users toggle between MIG, TIG, and flux‑cored modes via front‑panel buttons, with real‑time feedback on the LCD screen for precise control. and safety.OK!
Manual and Auto-Line Settings
The XMT 350 CC/CV offers two primary modes for controlling the welding arc: Manual and Auto‑Line. In Manual mode, the operator sets the desired amperage and voltage directly via the front‑panel knobs or the touch‑screen interface. The machine will maintain the selected values until the operator changes them or the arc is interrupted. This mode is ideal for experienced welders who prefer precise control over each weld pass.
Auto‑Line mode, on the other hand, automatically adjusts the output voltage to match the selected amperage and the workpiece condition. By selecting the appropriate welding process (MIG, TIG, or flux‑cored) and inputting the desired amperage, the inverter calculates the optimal voltage and maintains it throughout the weld. Auto‑Line also compensates for changes in material thickness, electrode angle, and wire feed speed, ensuring consistent weld quality without manual intervention.
To switch between modes, press the MODE button until the desired icon appears on the display. The machine will recalibrate the settings to match the chosen mode. Users can also fine‑tune Auto‑Line parameters by adjusting the voltage offset and current offset sliders, allowing for customization based on specific joint configurations or material types. The XMT 350 CC/CV’s intuitive interface and real‑time feedback make it straightforward to transition between Manual and Auto‑Line settings, providing flexibility for a wide range of welding tasks.
Real‑time display instant changes!
Welding Processes and Applications
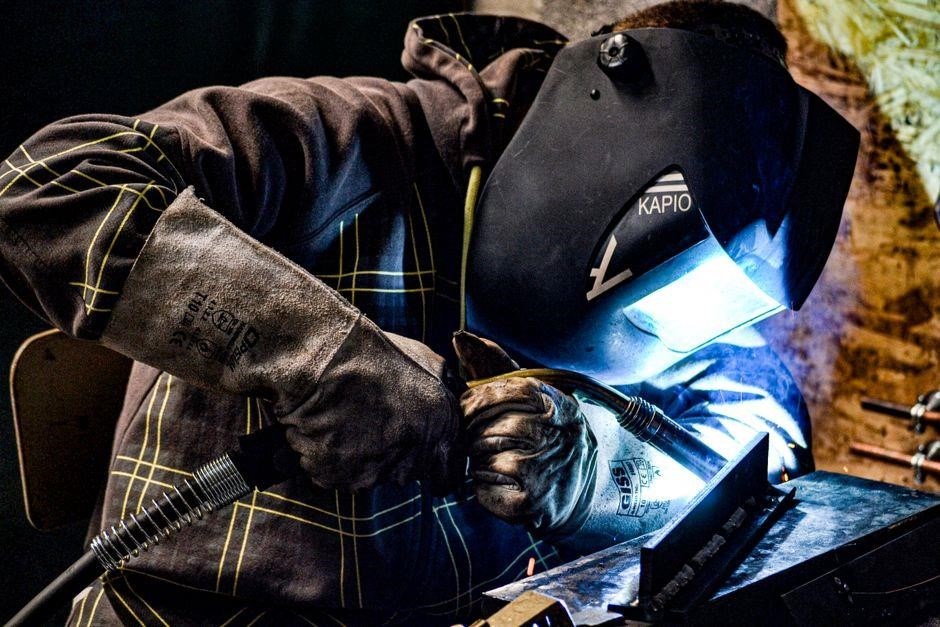
The XMT 350 CC/CV excels in MIG, TIG, and flux‑cored welding. Its Auto‑Line adjusts voltage automatically, ensuring consistent bead quality. Ideal for automotive, structural steel, and repair work, it delivers 30 A–350 A output with precise control and low noise.
Suitable for hobbyists and professionals.
MIG/MAG and Flux-Cored Welding
The Miller XMT 350 CC/CV delivers versatile MIG, MAG, and flux‑cored welding performance suitable for both light‑to‑heavy duty applications. Its inverter architecture provides precise voltage regulation, reducing arc instability and improving weld quality across a wide range of materials and thicknesses. The machine’s auto‑line feature automatically selects the optimal voltage and amperage for the chosen electrode or wire size, ensuring consistent penetration and bead appearance. Users can fine‑tune settings via the front‑panel controls or connect to a computer for advanced programming and data logging. For MIG welding, the XMT 350 CC/CV supports wire diameters from 0.023 to 0.080 inches, delivering smooth arcs and minimal spatter. Flux‑cored operation benefits from the built‑in gas‑less mode, allowing high‑speed production on ferrous and non‑ferrous materials without the need for shielding gas. TIG capability is also robust, with a 350 A maximum current and a 30 A minimum, allowing precise work on thin sheets or thick plates. The integrated gas‑less flux‑cored option eliminates the need for a separate gas supply, making the unit ideal for field jobs or remote locations. The built‑in cooling system maintains stable operating temperatures, even during prolonged high‑current runs. The user‑friendly interface displays real‑time arc parameters, and the adjustable duty cycle allows operators to balance productivity with equipment longevity. Preset tables for specific materials ensure repeatable welds across runs
Maintenance and Service
Routine maintenance for the XMT 350 CC/CV includes cleaning the air filter, inspecting the power cord, checking the cooling fan, and verifying the grounding strap. Replace worn filters every 100 hours, update firmware via USB to ensure optimal performance safety. Inspect the power cord for damage!Checkfan
Routine Maintenance Tasks
Regular upkeep of the Miller XMT 350 CC/CV guarantees reliable weld quality and prolongs the unit’s life. Perform the following tasks each month and after every 200 hours of operation:
- Inspect the power cord and plug: Check for fraying, cracks, or exposed conductors. Replace any damaged components immediately.
- Check the cooling fan: Verify that the fan runs at the correct speed and that the air vents are free of dust. Clean the fan blades with a soft brush if needed.
- Clean the electrode holder: Remove slag or residue that may hinder electrode contact. Use a non‑abrasive cloth and mild detergent.
- Verify the grounding strap: Ensure the strap is securely fastened to the chassis and that the connection is free of corrosion.
- Examine input and output terminals: Tighten any loose screws and clean contact surfaces with isopropyl alcohol.
- Update firmware: Download the latest firmware from Miller’s website and install it via the USB port to keep the inverter running at peak performance.
- Document maintenance: Record dates, observations, and any parts replaced in a maintenance log for future reference.
Adhering to these routine tasks minimizes downtime, prevents costly repairs, and keeps the welder operating within the manufacturer’s specified parameters.
For extended operation, inspect internal components such as the inverter board, capacitors, and heat sinks periodically. Use a multimeter to verify that the output voltage remains within tolerance. If you notice abnormal heat or noise, schedule a professional service visit.
When storing the machine for extended periods, disconnect the power supply, cover the unit with a breathable dust cover, and keep it in a dry environment to prevent moisture buildup.
Additionally, monitor weld quality by performing test welds on scrap material. Check for consistent bead appearance, penetration, and absence of porosity. Adjust settings if deviations are observed. Keeping a log of test results helps track performance trends over time.
Finally, replace consumables such as the electrode holder and grounding strap every 500 hours or when they show signs of wear. This proactive replacement strategy reduces the risk of weld defects and ensures safety during operation.
Troubleshooting Guide
When the XMT 350 CC/CV displays error codes, check the following: 1) Verify power supply voltage and grounding. 2) Inspect input cables for damage. 3) Reset the unit via the menu. 4) If the arc is unstable, adjust the wire feed speed. 5) Consult the manual for code definitions. Refer the wiring diagram!
Common Fault Codes and Remedies
When the XMT 350 CC/CV displays a fault code, the first step is to consult the code list on the back of the manual. Common codes include:
- F01 – Over‑current. Reduce welding amperage or check for a shorted electrode.
- F02 – Over‑voltage. Verify the input supply is within 115–125 V and that the transformer is correctly connected.
- F03 – Low‑input voltage. Inspect the power cord, connectors, and ensure the breaker is fully closed.
- F04 – Ground fault. Confirm the grounding strap is attached to a clean metal surface and that the earth connection is secure.
- F05 – Coil fault. Check for a damaged coil or loose solder joints on the PCB.
- F06 – Over‑temperature. Allow the unit to cool for 10 minutes; if the code persists, inspect the cooling fan and heat sink for dust or obstructions.
- F07 – Input line fault. Inspect the mains wiring for damage or a tripped circuit breaker.
- F08 – Output fault. Verify the welding cable and tip are correctly seated and free of corrosion.
- F09 – Control board fault. If the display shows a blank screen, reset the unit by disconnecting power for 30 seconds.
Reset the unit after correcting the fault; if it recurs, contact service.
Check parts for burnt traces, loose connections, damaged capacitors. Use a multimeter to check continuity. Replace failed components with OEM parts and log the fault code for reference!!